The plant's most expensive asset is also its most silent
The blast freezing tunnel decides the final quality of the product — core temperature, residence time, defrost condition — and shares none of it: proprietary controls, no network, ten to twenty-five years old. Replacing it costs hundreds of thousands and weeks of downtime. With Connect, an external camera aimed at the panel digitizes the freezing curve batch by batch without touching the equipment.
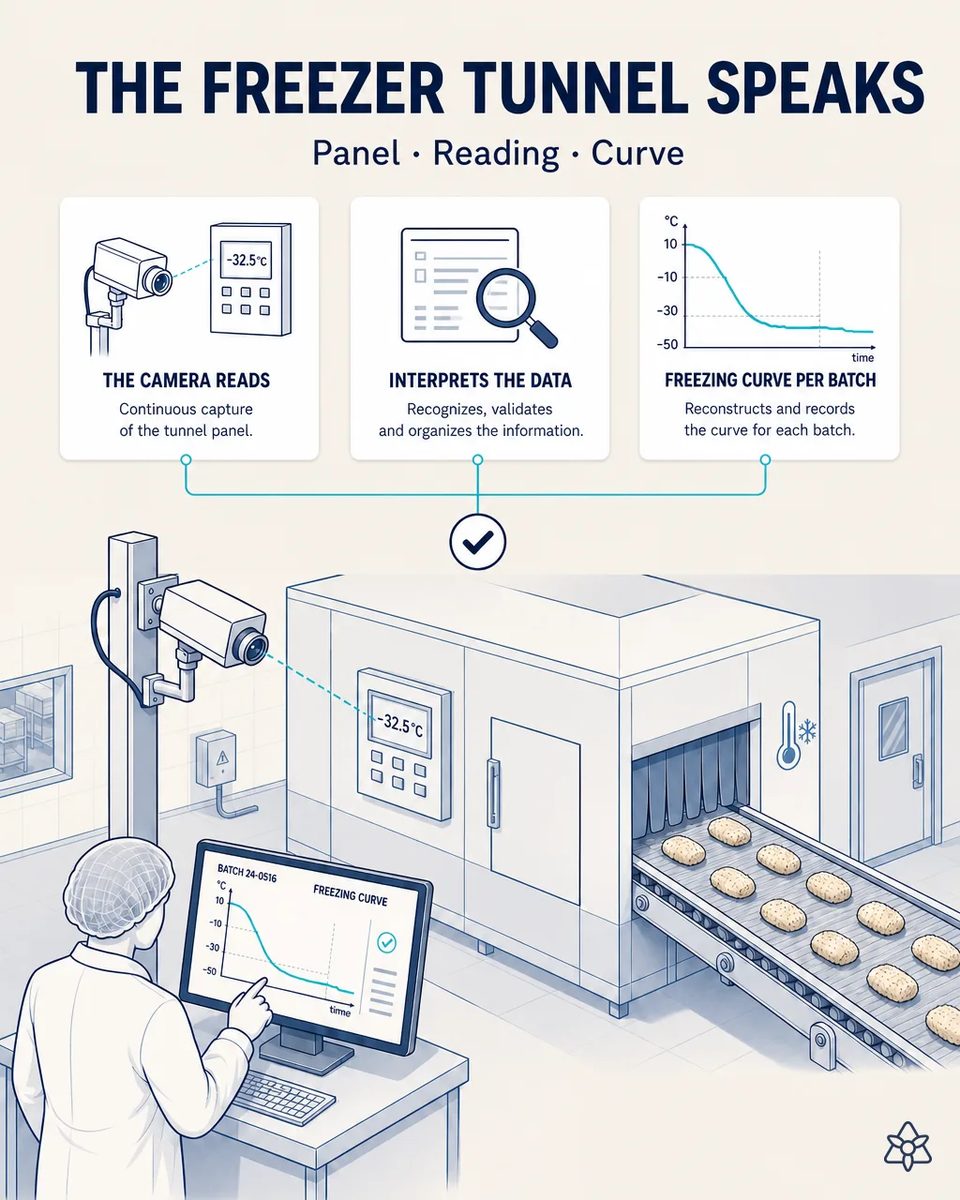
The machine that decides IQF quality is the one that shares nothing.
The IQF quality of a breaded product depends on a curve nobody logs continuously today: that the pieces come out loose rather than clumped, that the core reaches temperature, that the coating does not crack. What exists today is two or three manual readings per shift on a form. Enough to comply, not enough to understand. When a distributor returns a pallet for clumped product, there is no way to know what the tunnel did that night. And the obvious way out — replacing the equipment with a connected one — does not hold up: nobody replaces a blast freezing tunnel in order to obtain a data point.
- The blast or spiral tunnel decides whether the croquettes come out loose or clumped, whether the core reaches temperature, whether the coating cracks. It decides all of that and logs none of it: proprietary controls, no network, ten to twenty-five years old.
- What exists today is two or three manual readings per shift on a temperature form. Enough to satisfy the record, not enough to understand a bad night.
- When a retail distributor returns a pallet for clumped product, nobody can say what the tunnel did during that batch: the curve was on the panel for a few seconds and then it was gone.
- And the obvious way out does not hold up: nobody replaces a freezing tunnel worth hundreds of thousands, with weeks of downtime, to obtain a data point.
Connect in machine-panel photo mode — solved from outside, without opening the cabinet.
Connect in machine-panel photo mode.
It does not integrate with the tunnel's controller, opens no ports and installs nothing on the machine. On an asset this old and this critical, that is the difference between a case maintenance approves and a project nobody dares to authorize. And because every reading is tied to the work order that was inside the tunnel, the curve is not a machine log: it is a property of the batch, alongside its recipe and its lots.
- A fixed industrial camera with controlled lighting aimed at the panel.
- A vision model with grounded optical reading interprets every reading and builds the time series.
- The system cross-references the series with the active work order, so every stretch of the curve is tied to the batch that was inside the tunnel.
- The curve becomes available for root cause analysis and as an automatic audit record. The cabinet is never opened, the controller is never touched and the manufacturer's warranty is never voided.
Today's tunnel versus the tunnel being read
| Aspect | Today | With iLEAN Connect |
|---|---|---|
| The freezing curve | Two or three readings per shift | A continuous series per batch |
| A pallet returned for clumped product | "We do not know what happened" | Curve and complaint cross-referenced in minutes |
| Temperature record for the audit | A paper form | Automatic evidence tied to the batch |
| The tunnel's controller | — | Untouched, warranty intact |
| Replacement CAPEX | In the plan | Deferred indefinitely |
| Drift in the freezing process | Invisible until a complaint | Visible as a trend |
Impact estimate — to be validated with your numbers.
The block below is an estimate to be validated against your plant's actual data. We put it forward so the committee has an order of magnitude; we refine it during the assessment.
- Estimated payback 5-10 months.
- Indefinite deferral of the tunnel replacement CAPEX, which is the largest single investment line in a precooked frozen food plant.
- Fewer returns for freezing quality, because a curve that drifted is seen before the pallet leaves rather than after the distributor complains.
- And the temperature record for the audit goes from a form somebody fills in to an automatic series nobody has to defend.
estimated payback of 5 to 10 months, plus indefinite deferral of the tunnel replacement CAPEX and a reduction in returns for freezing quality. *Estimate to be validated*.
And the fair question from the production manager
“Does a camera reading a panel hold up in front of an auditor?” — here the task is anchored: a fixed screen, digits in a known position and a physically possible range, where the best models drop below 1.5% error [1]. The system discards any frame whose value falls outside the possible range instead of accepting it, so a glare or a hand in front of the panel never becomes a data point. And every reading keeps its original frame as evidence.
[1] OpenAI paper "Why Language Models Hallucinate", 2025 — on the reliability of AI in anchored tasks.
What people ask about reading the freezing tunnel panel
Do we have to touch the tunnel's controller?
No, and that is the point. The camera looks at the panel from outside; the cabinet is never opened, no software is installed and the manufacturer's warranty is never voided.
Does it capture the whole curve or just the set point?
The whole curve: what the panel shows at every moment, built into a time series and tied to the batch that was inside the tunnel at the time. The set point you already know; what is missing is what actually happened during the twenty minutes a tray of croquettes spent inside, and whether the core reached temperature before the outfeed.
Can we link a returned pallet to what the tunnel did?
Yes. The batch on the pallet label leads to the curve of that batch, so a return for clumped or cracked product becomes a root cause analysis in minutes instead of a shrug.
Does it work in a frozen environment?
The camera and its lighting are specified for the cold and the humidity of the tunnel area. It is a fixed industrial camera in a heated housing with its own controlled light, not a phone, so condensation on the panel and reflections from the stainless steel are handled at installation rather than in the model.
Does the same pattern work for other old machines?
Yes: pre-fryer, kettle, forming machine. You start with the tunnel because it is the most expensive, the most silent and the one that decides the quality of the finished product.
More cases from this series
- Non-conformities come from the gaps, not from the processEvery changeover and batch builds its dossier with photos, records and signatures, organized by…
- Four rings that verify each other, from recipe to palletFour verification rings cross-checking each other, from recipe to pallet, so the discrepancy is caught…
- The last machine to touch the product should not depend on typingLot, expiry and allergens travel from the work order to the coder by API, including in export market…
- Traceability is born on the dock, and it is born in a hurryPhotograph the delivery note, the lot labels and the thermometer: goods receipt enters the ERP after one…
- The person who knows the plant best is the one who can log the leastThe supervisor dictates while walking with both hands busy: iLEAN listens, ties it to the active batch…
- The good data lives in a spreadsheet the ERP never seesThe laboratory control sheet flows into the ERP after human sign-off, with up to 80% fewer licenses on…
Tell us how many readings per shift your tunnel record holds today.
We work on your plant's real data, not ours. Assessment with no commitment.
Request estimated ROI within 48h ‹ See all cases of precooked frozen foods See food industry