No line startup without visual evidence
A line switching tube gauge or OEM program requires readjusting and verifying every station before startup. Today that's closed with a human signature and no objective evidence. With iLEAN Edge, fixed cameras at every critical point compare the current state against the reference state. The line won't start until every camera reads OK and quality signs off on that evidence.
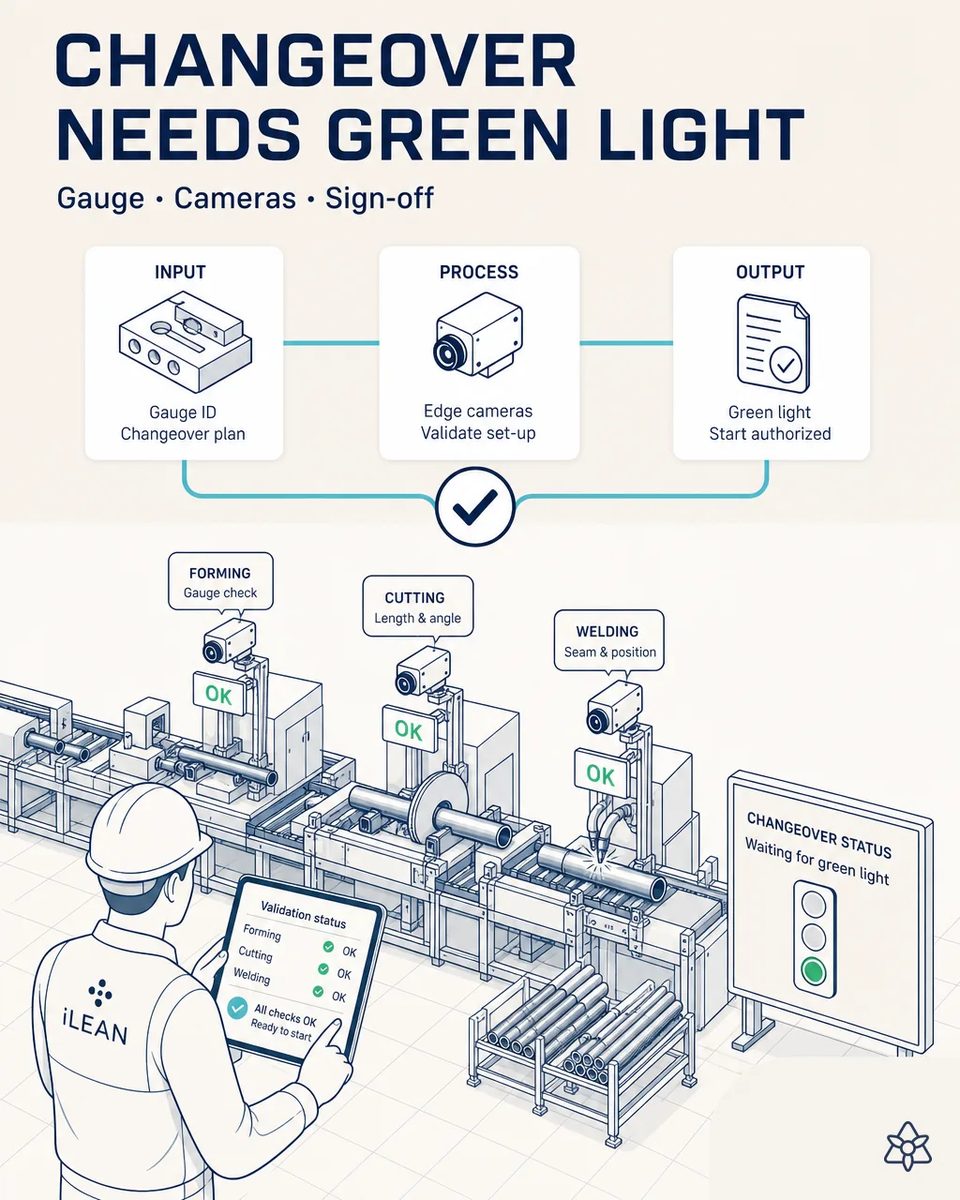
A gauge changeover closes on a signature with nothing behind it.
a gauge or program changeover stops the line for 1-3 hours and today closes on a human signature with no structured visual evidence — a direct risk under an IATF 16949 control plan.
- On a precision tube line, switching tube gauge or OEM program means readjusting forming stands, weld head position, sizing stands and the cut-to-length setting. The line stops for 1-3 hours, and everyone on the floor feels the pressure to restart.
- Today the changeover closes with a human signature and no structured visual evidence of the state of each station. The checklist is well designed; what fails is how it gets signed under time pressure.
- Under an IATF 16949 control plan that is a direct risk: a stand left at the previous setting can produce a whole out-of-tolerance lot, and a weld head a few tenths off the seam may pass the first-off piece and fail later.
- And when that happens, the investigation finds a signature, not a record of what the line actually looked like at startup.
Edge with JIDOKA AI — no green light, no startup.
Edge + JIDOKA AI. Industrial cameras with CNNs trained to recognize "ready vs. not ready" at each station. Startup blocked until OK + sign-off.
Each camera compares its station against the reference state for the new program. The line starts when all of them read OK and quality signs on that evidence: the decision stays human, the proof is new. And the more changeovers a line runs, the more the evidence is worth. High-mix lines, with several gauges a week, are where it pays first.
The signed changeover versus the evidenced changeover
| Aspect | Today | With iLEAN Edge |
|---|---|---|
| Forming stands after the change | Checked by eye | Compared with the new program's reference |
| Weld head and seam position | Assumed right | Confirmed by camera |
| Cut-to-length setting | Found at first inspection | Verified before startup |
| Quality sign-off | On trust | On images of every critical point |
| Out-of-tolerance first lot | A real possibility | Blocked at the source |
| Changeover record | A signature | Images, timestamps and signer |
a blind sign-off with risk of an out-of-spec lot → sign-off backed by visual evidence at every critical point.
Estimated impact — to validate with your own numbers.
The block below is an estimate to be validated against your plant's actual data. We put it forward so the committee has an order of magnitude; we refine it during the assessment.
- Payback set by your changeover frequency: we do not fix a month range, because the return is counted per gauge change, not per calendar month.
- Each blocked startup protects a whole lot that would otherwise run out of tolerance, with its scrap, sorting and possible containment.
- The sign-off stops being blind: it rests on visual evidence at every critical point.
- And the changeover record becomes evidence your control plan and your OEM can inspect, instead of a ticked box and no proof.
protection against a whole out-of-tolerance lot, payback depending on changeover frequency. *Estimate to validate*.
And the fair question from the production manager
“What if a camera holds the line for nothing, with the changeover clock already running?” — comparing a station against its reference state is an anchored task, where the best models drop below 1.5% error [1]. When the model is unsure, it does not block silently: it shows the image to the setter and quality decides. The line stops on a verifiable mismatch, not on a model's doubt. Every exception and every override is recorded with its author.
[1] OpenAI paper "Why Language Models Hallucinate", 2025 — on the reliability of AI in anchored tasks.
What people ask about validating the gauge changeover
Which points get a camera?
The ones your changeover procedure already treats as critical: forming stands, weld head, sizing and cut-to-length. They are chosen with your process engineer at commissioning. Most lines need three to five camera points.
How is the reference state for a new gauge created?
From a changeover done right, photographed station by station and approved by quality. Each gauge and program keeps its own reference set. When a program is revised, its reference is revised with it.
Does it add time to a changeover that already takes hours?
The check itself takes seconds per station. What it removes is first-lot scrap and the extra measuring done when nobody is sure of the setup. The changeover itself stays in your hands.
Can a changeover be released with one station not OK?
Only as a recorded exception signed by quality, with the image of that station attached. What cannot happen is a startup with no trace of who decided. Exceptions become visible in the monthly review.
Does it work when only the OEM program changes, not the gauge?
Yes. A program change can move the cut length or the weld setting without touching the stands, and the reference set for that program covers exactly those points. A same-gauge change is where a forgotten cut length slips through most often.
More cases from this series
- The travel card no longer gets lost on paperiLEAN Connect photographs the travel card at batch startup and makes the tube lot traceable in the…
- Talk to the AI without stopping your walkWith a headset, the line lead dictates issues hands-free; iLEAN structures and saves them within seconds.
- Zero hand-typed weld parametersiLEAN stitches the laser weld cell to the ERP: the correct parameter arrives on its own, with no manual…
- Two worlds that finally talk: spreadsheet and ERPiLEAN absorbs the dimensional-measurement spreadsheet in real time and uploads it to the ERP after…
- The truck no longer waits on your receiving dockOne photo of the delivery note and heat-lot labels is enough for iLEAN to push the data to the ERP after…
- No critical alert gets read too late againiLEAN catches steel delays and OEM specification changes at zero latency and suggests the specific…
Tell us how many gauge changeovers your lines run in a week.
We work on your plant's real data, not ours. Assessment with no commitment.
Request estimated ROI within 48h ‹ See all cases of precision automotive tubing See automotive