Your most expensive asset, connected without touching it
The tube mill that shapes the tube before welding is often 15-25 years old, with a proprietary panel and zero connectivity. Replacing it costs hundreds of thousands of dollars and weeks of downtime. With iLEAN Connect, one external camera aimed at the panel is enough: the machine stays the same, but now the plant has its forming parameters digitized batch by batch, without touching the original control.
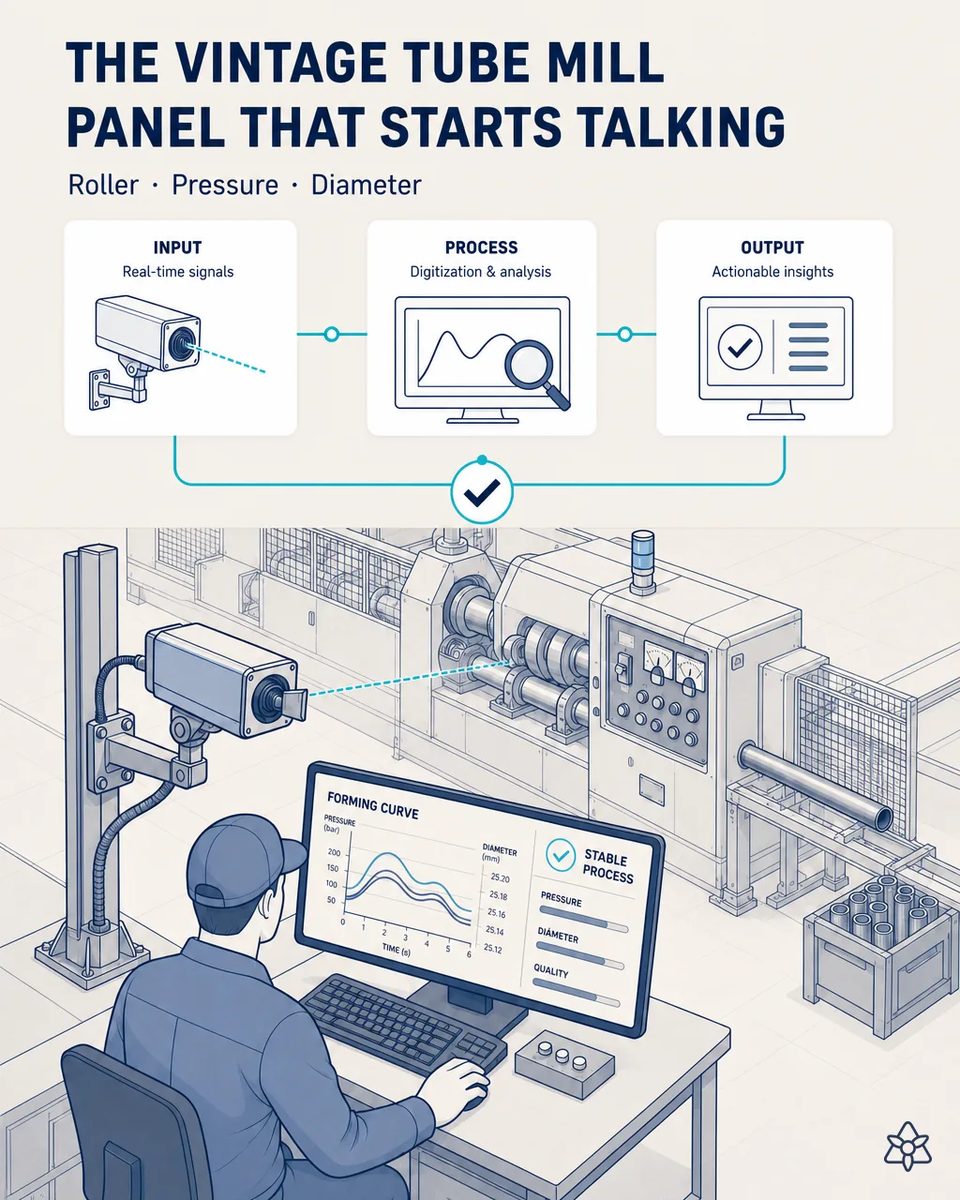
The data that explains an out-of-tolerance diameter dies on the screen.
The tube mill is a physical bottleneck and one of the most expensive assets to replace. Its panel holds the information that would explain why a batch comes out with an out-of-tolerance diameter deviation, but that data dies every time the screen changes view.
- The tube mill shapes the strip through its forming stands before the seam is welded. It is often 15-25 years old, with a proprietary panel and zero connectivity.
- Replacing it costs hundreds of thousands of dollars and weeks of downtime, so it stays — and it stays blind. It is the physical bottleneck of the line, and everything downstream depends on how it formed the strip.
- Its panel shows roll pressure, line speed and the readings that would explain why a batch comes out with an out-of-tolerance diameter deviation. Each time the screen changes view, that value is gone.
- So when sizing or final inspection finds ovality or diameter drift, nobody can tie it back to what the forming stands were doing at the time. The 8D ends with a probable cause instead of a proven one.
Connect in photo mode on the panel — nothing is wired into the machine.
Connect photo mode over the panel. Fixed industrial camera. OCR with a grounded LLM interprets each reading, structures it into a time series per batch, and cross-references it with the active ERP program.
The machine stays exactly as it is: same control, same panel, same operator. What changes is that every reading it shows becomes a time series tied to the batch and the ERP program, and root cause stops being a guess. On the most expensive asset in the plant, that is the difference between an approvable project and one nobody dares to start.
The blind tube mill versus the tube mill being read
| Aspect | Today | With iLEAN Connect |
|---|---|---|
| Roll pressure and line speed | Visible only while on screen | Time series per batch |
| Diameter deviation at sizing | Found with no cause attached | Crossed with the forming readings |
| Root cause for a batch | Days of guessing | Minutes |
| The original control | — | Untouched, no ports opened |
| Scrap from out-of-range forming | Counted after the fact | Traced to the stand reading behind it |
| Replacing the tube mill | On the CAPEX list | Deferrable indefinitely |
zero correlation between forming parameters and downstream defects → root-cause analysis per batch in minutes. Machine replacement becomes indefinitely deferrable.
Estimated impact — to validate with your own numbers.
The block below is an estimate to be validated against your plant's actual data. We put it forward so the committee has an order of magnitude; we refine it during the assessment.
- Estimated payback 5-10 months.
- Avoided replacement CAPEX, which for a tube mill runs to several hundred thousand dollars, plus the weeks of downtime a replacement would cost.
- Less scrap from out-of-range forming, because the reading behind it is finally on record and can be acted on before the next batch.
- Root cause per batch goes from zero correlation between forming and downstream defects to an answer in minutes.
estimated payback 5-10 months, avoided replacement CAPEX (several hundred thousand USD), reduced scrap from out-of-range forming. *Estimate to validate*.
And the fair question from the production manager
“Can a camera reading an old panel be trusted in front of an OEM?” — the task is anchored: a fixed screen, values in known positions and physical ranges your process engineer already knows, where the best models drop below 1.5% error [1]. Any reading outside the physically possible range is discarded rather than stored, so the series you show a customer holds only plausible values. And the operator never has to write a reading down again.
[1] OpenAI paper "Why Language Models Hallucinate", 2025 — on the reliability of AI in anchored tasks.
What people ask about reading the tube mill panel
Does anything get installed on the tube mill's control?
No. The camera sits on its own bracket in front of the panel. No software, no cable and no port on the original control, so nothing about the machine's behavior changes. Its validation and its warranty stay as they are.
What if the panel has analog gauges as well as a screen?
Both are read. Needle gauges and digital displays are just different fields in the same image, and each one is mapped once at commissioning. If the operator switches screens, the camera reads whichever view is showing.
Does it help with ovality and straightness complaints?
That is where it pays most: with the forming readings stored per batch, a drift in ovality at sizing can be traced to the stand that caused it. That turns a complaint into a concrete adjustment instead of a general recalibration.
How is each reading tied to the right batch?
Through the ERP program active at that moment. Every reading carries a timestamp and the running program, so the series belongs to a batch, not just to a clock. Coil changes mid-batch show up as their own segment.
Is it worth it if the tube mill will be replaced one day?
Yes, because it pays within months, and the data it gathers is exactly what you need to specify the next machine well. Many plants find the replacement can wait far longer than planned.
More cases from this series
- The travel card no longer gets lost on paperiLEAN Connect photographs the travel card at batch startup and makes the tube lot traceable in the…
- Talk to the AI without stopping your walkWith a headset, the line lead dictates issues hands-free; iLEAN structures and saves them within seconds.
- Zero hand-typed weld parametersiLEAN stitches the laser weld cell to the ERP: the correct parameter arrives on its own, with no manual…
- Two worlds that finally talk: spreadsheet and ERPiLEAN absorbs the dimensional-measurement spreadsheet in real time and uploads it to the ERP after…
- The truck no longer waits on your receiving dockOne photo of the delivery note and heat-lot labels is enough for iLEAN to push the data to the ERP after…
- No critical alert gets read too late againiLEAN catches steel delays and OEM specification changes at zero latency and suggests the specific…
Tell us how old your tube mill is and what its panel shows that nobody records.
We work on your plant's real data, not ours. Assessment with no commitment.
Request estimated ROI within 48h ‹ See all cases of precision automotive tubing See automotive