It doesn't start until the configuration is verified
A line assembling switchgear across different ratings in the same shift needs to verify, before starting each order, that the cell is correctly configured. With iLEAN Edge, fixed cameras at every critical point compare the current configuration against the reference and block startup until validated.
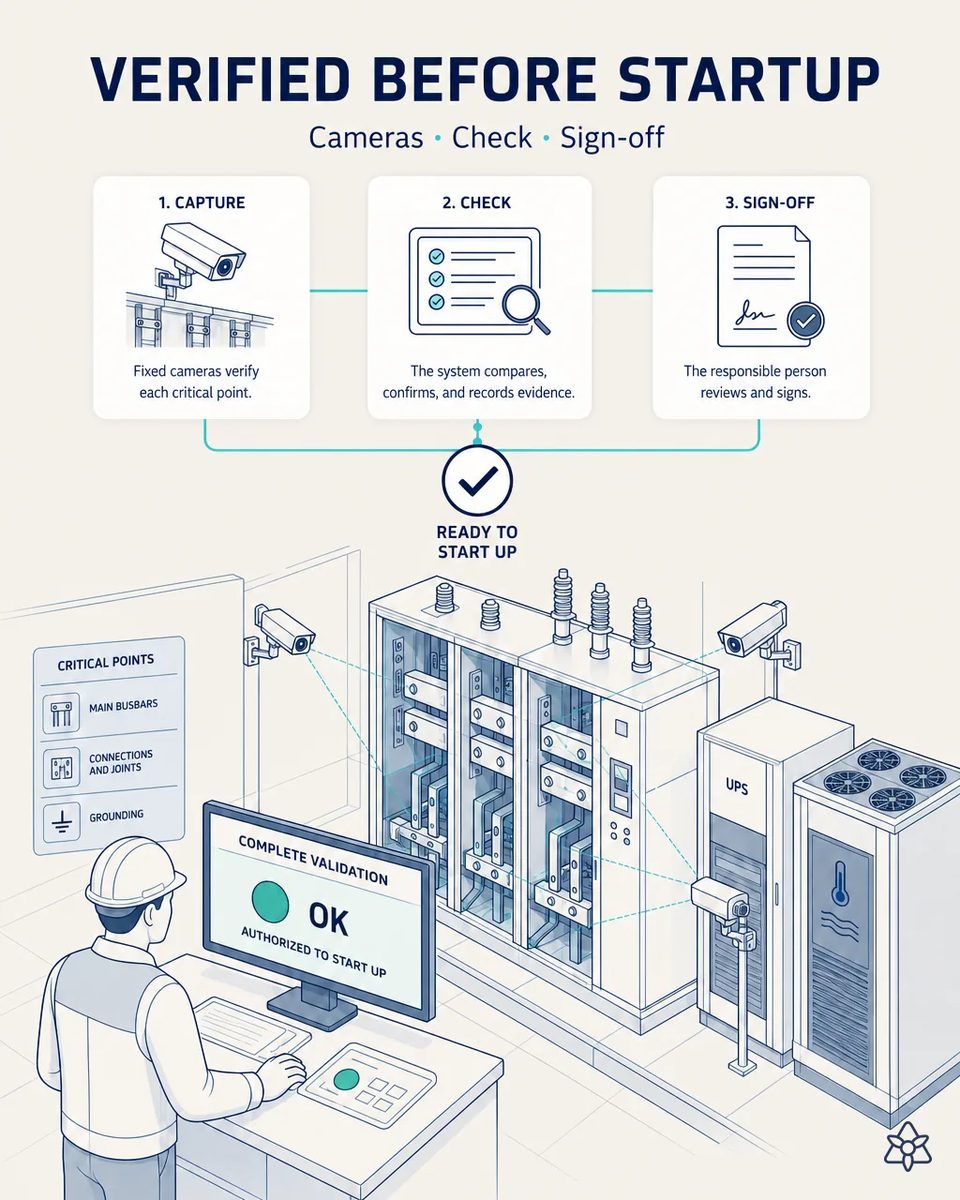
A wrong busbar setup is an electrical safety risk signed off with a tick.
A wrong busbar configuration in medium-voltage equipment isn't a cosmetic defect, it's an electrical safety risk — and today it rests on a technician signing off "correctly configured" with no objective visual evidence.
- The same line assembles switchgear of different ratings in the same shift. Before each order, the cell has to be set up correctly: main busbars, joints, phase spacing, grounding. Each rating has its own drawing, and the differences between them are sometimes a few millimeters.
- A wrong busbar configuration in medium-voltage equipment is not a cosmetic defect. It is an electrical safety risk, and potentially an out-of-spec unit shipped as conforming.
- Today that risk rests on a technician signing “correctly configured” on a checklist, with no objective visual evidence behind the signature and the next order already waiting.
- When something goes wrong, the investigation finds a signed box and nothing else. It is not bad faith: a signature is not evidence, and under time pressure it never will be.
Edge with JIDOKA AI — assembly does not start until the cameras read OK and quality signs.
Edge + JIDOKA AI. Industrial cameras with CNNs trained to recognize "correct configuration vs. deviation" for each rating. Assembly can't start until every camera reads OK + the quality lead signs off with evidence.
The cameras do not decide alone. They compare each critical point with the reference for that rating, and the quality lead signs on that evidence. What changes is not who approves the start, but what they approve it on — and that the evidence stays attached to the order.
The rating changeover today versus the changeover checked by camera
| Aspect | Today | With iLEAN Edge |
|---|---|---|
| Busbar configuration sign-off | A tick on the checklist | Every critical point compared with its reference |
| Phase spacing and joint layout | Checked by eye | Read by fixed cameras per rating |
| Grounding connection | Assumed from the drawing | Confirmed before startup |
| Start of assembly on a wrong setup | Possible under time pressure | Blocked until OK and signature |
| Evidence of the busbar setup afterwards | A signed box | Images stored with the order |
| Ratings mixed in one shift | More changeovers, more exposure | Each changeover verified the same way |
A blind sign-off with configuration risk → a sign-off backed by visual evidence at every critical point.
Configuration validation: impact we estimate with you, changeover by changeover.
The block below is an estimate to be validated against your plant's actual data. We put it forward so the committee has an order of magnitude; we refine it during the assessment.
- Payback varies with how often your configuration changes: we do not fix a range because it depends entirely on your ratings mix per shift and on what one incident would cost your plant.
- It protects against an electrical safety incident or an out-of-spec unit, whose cost far exceeds a few minutes of line downtime at each changeover, and against the investigation that follows either one.
- The sign-off goes from blind to backed by visual evidence at every critical point, and the quality lead signs knowing what they are signing.
- And when a customer or an auditor asks how a unit was configured, the images exist with its order instead of a tick on a sheet. The answer takes a minute, and it is evidence, not a recollection.
Variable payback depending on how often configuration changes occur; protects against an electrical safety incident or an out-of-spec unit, whose cost far exceeds a few minutes of line downtime. *Estimate to validate.*
And the fair question from the production manager
“What if the cameras block the line over nothing?” — that is the right objection, because changeovers sit on the shift's critical path. Comparing a busbar layout against its stored reference is an anchored task, where the best models drop below 1.5% error [1]. When the camera is unsure it does not block silently: it escalates to the quality lead, who decides on the evidence in front of them.
[1] OpenAI paper "Why Language Models Hallucinate", 2025 — on the reliability of AI in anchored tasks.
What people ask about validating busbar configuration before startup
Which points do the cameras check?
The ones your engineering defines as critical for each rating: main busbars, joints and spacing, grounding and any barrier that changes between configurations. The list is agreed at commissioning and can grow as incidents teach you where the risk is.
How much time does the check add to a rating changeover?
Seconds. What adds time today is the extra margin people take because there is no evidence, the second look and the call to the quality lead, and that margin is what disappears.
Can the check be skipped when the line is behind?
An exception can be approved with the quality lead's signature, and it is recorded as such. Starting with no trace of who skipped it is what stops being possible, and that alone changes how often the exception is used.
What happens when a new rating is introduced?
Its reference images are captured once on a correctly built unit and validated by engineering, and from then on it is checked like the others. No retraining project is needed for each new rating, which matters when data-center customers keep asking for new configurations.
Why is there no payback range on this case?
Because it depends on how many changeovers you run and what an incident would cost you. We estimate it with your own mix rather than quote a generic figure that would not hold for a plant running two ratings a week or ten a shift.
More cases from this series
- The assembly traveler no longer gets lost in paperHow a switchgear factory digitizes its paper assembly traveler with a photo, no habit change.…
- The truck no longer waits while someone typesOne photo of the delivery note and the critical-component certificate is enough to clear the truck and…
- The supplier alert no longer waits hours in an inboxILEAN reads a critical-component supplier's email at zero latency and replans the line before material…
- Nothing enters the central system without a human validating itNothing enters the ERP without a technician validating it with two taps. That's how iLEAN avoids…
- The supervisor's knowledge no longer dies at end of shiftWith an earpiece and Connect, the line supervisor logs incidents while walking between stations — no…
- The lab spreadsheet no longer lives cut off from the ERPILEAN absorbs the lab's test-result spreadsheet in real time and pushes it into the ERP. Up to 80% fewer…
Map with us the critical configuration points of each switchgear rating you build.
We work on your plant's real data, not ours. Assessment with no commitment.
Request estimated ROI within 48h ‹ See all cases of critical datacenter infrastructure See electronics