The assembly supervisor dictates on the move
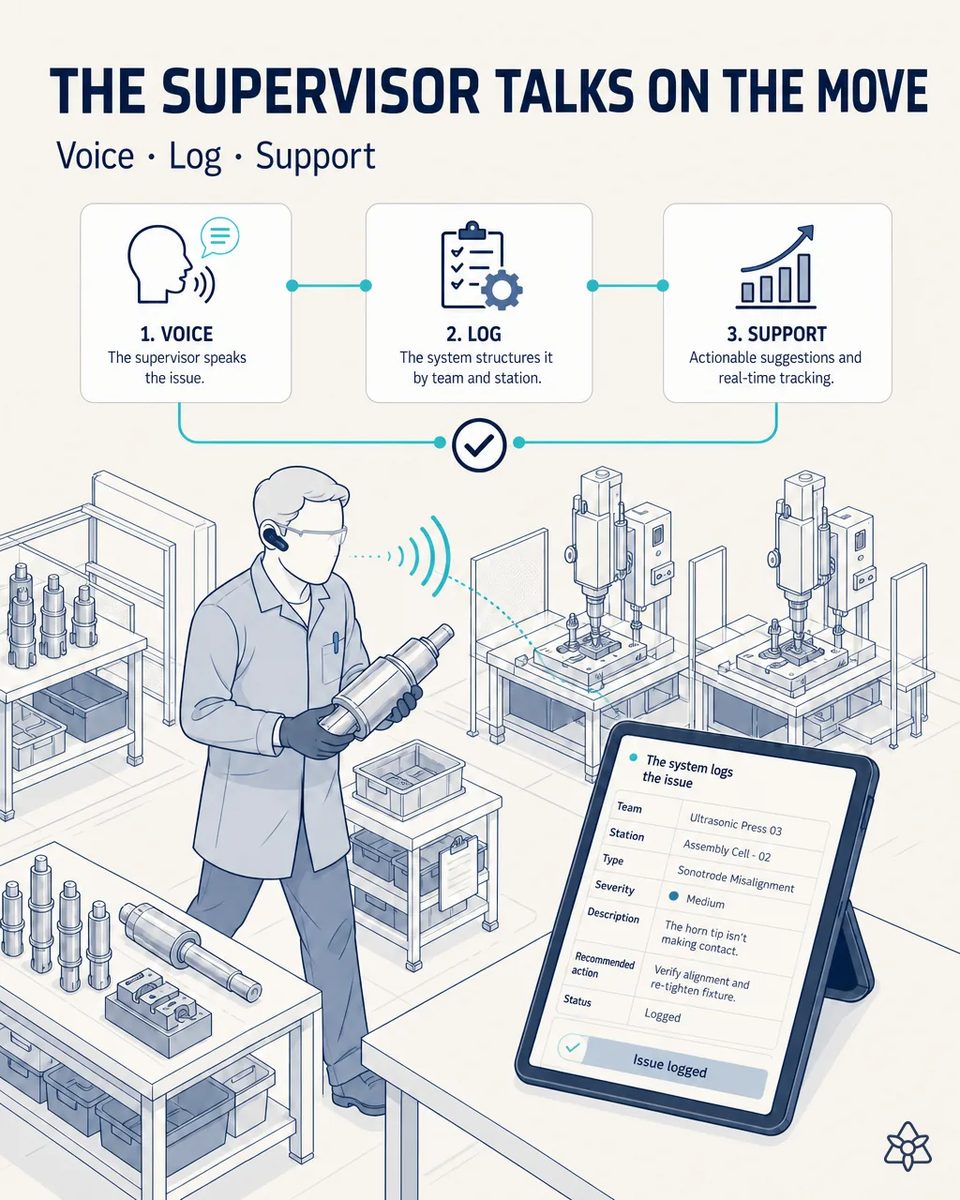
The assembly supervisor spends the shift moving between cells: adjusting an actuator, checking a tuning, holding a transducer. With busy hands, nothing gets logged. That the latest batch of piezo ceramics is more fragile, that a machine is waiting for a booster, that the new technician needs support: it all stays in their head. With iLEAN Connect in earpiece mode they say: note that the press for the automotive order is waiting for the 1:1.5 booster. iLEAN structures it as an issue linked to the machine and the order.
The most valuable information on the assembly floor lives in one person's head.
The assembly supervisor spends the shift moving between cells: adjusting an actuator, checking a tuning, holding a transducer. With busy hands, nothing gets logged. That the latest batch of piezo ceramics is more fragile, that a machine is waiting for a booster, that the new technician needs support: it all stays in their head.
- The assembly supervisor spends the shift between cells: adjusting a pneumatic actuator, checking a tuning, holding a transducer while a technician torques the stack.
- With both hands busy, nothing gets logged. There is no free hand for a terminal and no time to write it at the end.
- That the latest batch of piezo ceramics seems more fragile, that a press is waiting for a 1:1.5 booster, that the new technician needs support on generator wiring: it all stays in their head.
- At shift change part of it is passed on verbally, and part of it is simply lost. Continuous improvement never sees the recurring issue because it was never written down.
Connect in earpiece mode — the supervisor talks, iLEAN structures and answers.
With iLEAN Connect in earpiece mode they say: note that the press for the automotive order is waiting for the 1:1.5 booster. iLEAN structures it as an issue linked to the machine and the order. iLEAN alerts purchasing and replies by voice: the warehouse confirms the booster at noon. The supervisor stays in command; AI simply takes the keyboard off their hands.
The supervisor does not fill in anything: they say what they would have said to a colleague. iLEAN turns it into an issue linked to the right machine and order, and replies by voice when someone else, like purchasing or the warehouse, answers. The keyboard leaves their hands; the command stays with them. The next shift starts with the open issues per machine, not with a hallway summary.
Issues in the supervisor's head versus issues logged by voice
| Aspect | Today | With iLEAN Connect |
|---|---|---|
| Press waiting for a booster | Mentioned at shift change, maybe | Issue on that serial, purchasing alerted |
| Fragile piezo ceramics batch | A hunch nobody records | Logged against the ceramics lot |
| Where the supervisor's hands are | On the stack, not on a keyboard | Still on the stack |
| Reply from the warehouse | Supervisor walks to ask | Spoken back in the earpiece |
| Shift handover in assembly | Verbal and partial | Open issues per machine |
| What continuous improvement receives | Anecdotes from the floor | Recurring issues with dates |
Before: knowledge lost at shift end. After: issues logged in real time.
Impact estimate — to be validated with your numbers.
The block below is an estimate to be validated against your plant's actual data. We put it forward so the committee has an order of magnitude; we refine it during the assessment.
- No standalone payback: this is an enabling piece, and we do not put a number on it by itself because its value depends on how many issues get lost today.
- What it does is make shop-floor knowledge enter the system in real time instead of disappearing at shift change.
- All continuous improvement depends on this information existing: a fragile ceramics lot or a booster that is always late only becomes a pattern once it is written down.
- We size it with your continuous improvement team, and it feeds the flagship case, where the supervisor's issues become one more signal about which order is at risk.
Enabling value · shop-floor knowledge enters the system in real time (estimate to be validated). Hard to price upfront, but all continuous improvement depends on this information existing. Enabling value; an estimate to be validated with the CI team.
And the fair question from the production manager
“Will my assembly team feel listened to all day?” — no. iLEAN only records after the wake word and only the supervisor's voice, never the technicians' conversations. On reliability, turning a short dictation into machine, order, component and issue type is an anchored task where the best models drop below 1.5% error [1], and the structured note is read back for the supervisor to confirm before it is stored.
[1] OpenAI paper "Why Language Models Hallucinate", 2025 — on the reliability of AI in anchored tasks.
What people ask about the assembly supervisor's earpiece
Does it work with the noise of presses and compressed air?
Yes. The earpiece uses a close-talk microphone designed for noisy floors, and it is commissioned with the real noise of your assembly hall and test area. Ultrasonic test runs and air blow-off are part of that commissioning, not a surprise afterwards.
How does it know which machine the supervisor means?
From what is said, such as the order, the customer or the serial, cross-checked with the machines currently in assembly. If two machines match, it asks back by voice before logging anything. A wrong link is worse than no link, so it prefers to ask.
Can the supervisor ask questions, not just dictate?
Yes. They can ask whether the booster for an order has arrived or which machines are waiting for a generator, and get the answer spoken back without leaving the cell. The answer comes from the same memory the planners see, so nobody gets a different version.
Does it understand terms like booster ratio, stack or amplitude?
Yes, the vocabulary of the plant is loaded at commissioning: component names, ratios, frequencies and the nicknames your team really uses for each cell. New terms are added as they appear, without retraining the whole system.
How do you value an earpiece case that has no payback range?
By what it feeds: the issues it captures are the input for continuous improvement and for the flagship case. We size that with your continuous improvement team rather than print a generic range. In practice, it is approved together with the cases it feeds.
Tell us how many issues your assembly supervisors carry in their heads each shift.
We work on your plant's real data, not ours. Assessment with no commitment.
Request estimated ROI within 48h ‹ See all cases of ultrasonic welding equipment See metal fabrication and capital equipment